Tag Archives: SMT assembly

Importance of Good ESD Practices in SMT Assembly

The management of electrostatic discharge is a crucial feature in the production, assembly, and maintenance of electronic equipment. If electrostatic discharges are not managed, they may destroy an electrical device at any step of its manufacture or use. Grounding any wires that come into touch with or are close to the electrical equipment is the main way of control. Humans, tools, ESD mats, various electronic equipment, boards, connections, packing, and other conductors are among them. Removal of extra insulators, shielding, ionization, pollution regulations, training, awareness, and highest level compliance are all part of a successful ESD management program.

What exactly is ESD?

The quick current flow between two oppositely charged objects generated by the response to an electric short or insulator breakdown is known as electrostatic discharge (ESD). Tribocharging via electrostatic induction may generate a build-up of high voltage. When different-charged items are placed near together, or the dielectric among them disintegrates, ESD develops, which typically results in a vivid spark. This could result in major part damage during the printed circuit board assembly process.

ESD may generate tremendous electric sparks and less dramatic forms, not seen or heard but strong enough for sensitive electrical equipment to be harmed. Electric sparks need a field strength in the air of more than 40 kV/cm, as seen in lightning strikes. Energy transfer from acute electrodes and brush discharge from flat electrodes are two further types of ESD.

Smt assembly
Smt assembly

What is the importance of ESD?

Exposure to ESD, or the abrupt passage of electricity over two electrically charged items, may cause any electronic device or part to deteriorate. When two differentially charged items brush against one other, an apparent spark is typically produced. Even easy movement on a workstation may cause ESD, which may harm a device’s sensitive electrical components. It may also have an impact on the functioning and quality of electrical devices and components. As a result, ESD protection solutions are critical for preventing the accumulation of electrostatic force in electronic devices. Their primary purpose is to limit the possibility of ESD-sensitive equipment being damaged. These protective solutions are particularly successful in preventing system failure and extending the life of fragile electrical devices.

A pro-EPA (ESD protected area) should be established for the safety of production facilities or pcb assembly workstations. EPA may be enhanced using ESD-resistant goods, including workbenches, commercial furnishings, trolleys, warehouses, etc. Wristbands, conductive straps, and other devices may be worn by persons working in the vicinity to safely disperse ESD. These items are wired to the ground, where an electrostatic charge is dissipated via earthing points and connections. This allows ESD to be dissipated more safely.

ESD Protection Zones in the Facility:

Electrostatic Discharge Shielded Locations (EPAs) prevent ESD-sensitive devices from typical electrostatic discharge sources by grounding conductive objects and personnel in ESD-prone production areas such as:

Pro mats, for example, are conductive surface materials.

  • Staff uniforms and clothing with conductive filaments
  • Optimal humidity levels

Circuits with built-in ESD protection:

When assemblies are most susceptible like during electronic assembly, built-in ESD protection decreases the danger of complete circuit breakdown or latent damage. The following are some of the best practices for ESD protection built-in:

  • Choosing the right short backflow prevention device for your Printed Circuit Board
  • Installing the isolator at the ESD contact site

What is ESD (Electronic Stability Device) Training?

Controlling electrostatic discharge requires ESD training. You recognize the significance of avoiding electrostatic discharge. You already know that in electronics assembly, an ESD control program is critical for quality and yield. Any successful ESD control program and vital to successful electronic manufacturing require an effective, systematic, and long-term ESD training, certification, and re-certification system.

What is ESD 20.20 Training?

Electro Static Discharge (ESD) is a typical phenomenon in which a person or almost any ‘charged’ item emits a brief electrical shock.

The multi-industry guideline for developing ESD management programs that safeguard today’s highly sophisticated electrical parts, assemblies, and machinery from expensive ESD damage and decrease downtime is ANSI/ESD S20.20. An organization may design an ESD control program that protects equipment down to 100 volts or fewer using the format’s control techniques and advice.

The S20.20 standard, which several multinational OEMs use and serve as a successor for MIL-STD 1686, has swiftly gained traction in the electronic, telecommunications, aircraft, automotive, and devices sectors. In reality, the S20.20 standard is included in the telecom industry reference TL 9000 as a recommended practice for addressing ESD control requirements.

A good ESD management program within a printed circuit board assembly facility may help you avoid expensive system failures while also improving customer service. Organizations may use NQA’s ESDA-accredited Site Certification program to guarantee that their programs satisfy the standards and give documentation of conformance for customer marketing reasons.

When it comes to ESD training, there’s a statement that goes something like this:

“Managing an ESD program is an important aspect of a full quality program in the modern electronics sector. Any electronics company that does not have an active ESD program is putting itself or its customers in danger.”

At PNC, all the employees receive annual ESD training based on ESD 20.20.

What Are the Advantages of ESD Training?

Improper handling of today’s electrical components may quickly harm or make them faulty. Furthermore, rejecting or fixing items affected by electrostatic discharge (ESD) may waste time and money for companies that handle electronic components.

  1. Raises ESD awareness in the workplace
  2. Enhances overall performance levels and product control
  3. Lowers the failure rate, lowers rework, and saves money.
  4. Aligns with peers in the electronics industry
  5. Provides consumers with clear evidence during site visits
  6. Controls for ESD (proper clothing, grounded tables, signage, etc.)
  7. Increases marketability and gives you a competitive edge.

What is ESD Audit?

A solid ESD control program should include an ESD audit. It audits all ESD-control processes and products, reminds employees of their obligations regularly, and provides management with the information needed to take remedial action.

An audit is conducted using an ESD control program that has been designed, authorized by management, and applied at all levels of the smt assembly area. In most cases, such software is based on industry-developed standards. ANSI/ESD S20.20-1999, produced and regulated by the ESD Association, is the cost of setting up a document for many programs and is a good option for a guiding standard.

ESD Audit Work Area:

The audit must ensure that the border between ESD-protected and non-ESD-protected locations is properly marked, e.g. signs, directional arrows, and floor markings. This reminds both employers and employees that they enter a critical control environment or leave it.

Supply carts to store or carry ESD-sensitive items should have electrically linked uprights and shelves mounted by a trailing chain to avoid tribo-loading. A floor snap is strongly suggested for strong grounding of the cart when fixed in an ESD safe location.

ESD Practices at PNC Online                           

During an audit at PNC, it was noted that all the employees themselves tested multiple times a day. The company follows all standard patterns for complete ESD audits on an annual basis. PNC employees wear ESD Smocks, wrist straps, foot Straps, and ESD shoes.

What’s a HDI Printed Circuit Board?

HDI stands for High Density Interconnect. HDI PCBs have finer traces and trace spacing, laser drilled micro vias and higher connection pad density. Its two chief advantages are that it permits the use of fine pitch BGAs and it reduces the number of PCB layers required because the finer traces and smaller vias allow more circuitry in a smaller area.

Narrow trace widths mean higher circuit density

At PNC standard PC Board fabrication uses a minimum trace width of 5 mil, with a 5 mil space between traces (5/5mil) PNC’s HDI trace widths can be as narrow as 3 mil with 3 mil spacing.  These finer traces allow 160% more traces in the same real estate. 3/3mil spacing will also allow two traces to escape between pads of a standard BGA, meaning less PCB layers are needed to fan out the pins from the BGA.

Microvias are the enabling technology for HDI

Narrow trace widths used in HDI PC Board are a result of the gradual refinement of photolithography and etching technology.  Microvias on the other hand, are a revolutionary innovation driven by the development of high powered lasers that can be controlled accurately enough to ablate a 3 mil hole through the surface layer of copper and underlying laminate, without damaging the underlying layer of copper.

The minimum hole size for PNC’s laser drilled microvias are 3 mil and the minimum pad diameter for the microvia is 7 mil.  Pads for laser drilled holes can be smaller than for mechanically drilled holes because of the location accuracy of the laser drilled hole.  There is no mechanical deflection of the drill bit to account for.  The laser drilled holes can be fully copper filled and planarized flat, so they can be used as pads for fine pitched BGAs with 0.4mm or smaller spacing. Using microvias as pads allows the signal trace to fan out by going straight down and out to an inner layer of the printed circuit board.

The biggest limitation with microvias is the aspect ratio of the holes.  Where a drilled through hole can have a 10:1 depth to diameter aspect ratio, a laser drill can achieve no more than around a 1:1 aspect ratio.  This means that the smallest microvia can only connect two adjacent copper layers. A larger diameter microvia can penetrate two layers. To connect deeper layers, the designer must stack vias one directly atop another.

Laser drilling of the microvias changes the way PCBs are fabricated and gives the designer flexibility that they do not have with through hole vias.  In a standard drilled PCB, via holes are drilled and plated after the PCB fabrication stack-up is completed.  Because the microvias can only bridge two or three copper layers, the microvias must be drilled and plated at each lamination step.  This means that microvias can be fully buried between layers, stacked or staggered to allow the microvia to connect multiple layers of the stack up.

The major space saving advantage of the microvia technology is that vias can just connect traces that need to be connected, rather than taking up real estate all the way through the PCB the way a through hole via does.

The Printed Circuit Board designers at PNC take advantage of this by locating the power and ground layers at the top of the stack up.  Since all active components access power and ground, sometimes through multiple pins, having the power and ground layers directly below the component layer allows all those connections to be made directly by microvias.  This leaves the component layers and layers beneath the power and ground layers completely unobstructed for signal routing. This has the added advantage of reducing parasitic capacitance because it eliminates the circuit stubs caused by plated through holes.

Two sided boards are typically fabricated with a combination of through holes and microvias.   Though holes can be drilled just through the core, connecting the stacks on the top and bottom of the board from the lowest layer, or through holes can be drilled through the entire stack directly connecting the traces on the top and bottom component layers.


HDI PCBs are a necessity when using fine pitched BGAs, but they can also reduce cost on PCBs without fine pitched BGAs because of the reduced layer count.  On your next PCB design, talk to the experts at PNC.  They can help you determine if HDI technology is can reduce your PCB cost by reducing layer count and shrinking the PCB size.

PCB assembly Pre-Reflow FAI

First article inspection (FAI) prior to SMT assembly is a design verification methodology that provides a reported verification and validation of details of a product on the shopfloor per its manufacturing procedure and requirements. There are various ways to perform FAI, from both supplier’s and customer’s side, making it a very dynamic process. This means that each organization can tailor its FAI method to benefit itself and consequently, its customer, yet maintain rigid performance standards at the same time. FAI involves qualitative and quantitative measurement. FAI is also highly effective since it can potentially fulfill process validation requirements of quality management systems like ISO9001 or AS9100.

In the PCBA manufacturing industry, FAI can be effectively employed in validating materials for manufacture, underlying technologies, manufacturing processes used, packaging, and equipment. It can also be applied to a batch of a given sample-size from a mass-production instead of just the first sample, as the name might suggest. At PNC, strict adherence to our manufacturing standards helps in production with better yield but at the same time, facilitating dynamic validation techniques in our manufacturing process allows us to reduce lead time. The focus of FAI in PNC assembly lies in validating the pcb assembly before reflowing so that the SMT team can make necessary adjustments for the next batch, saving time and effort during rework. They are also responsible for validating the correct loading of the right component in its allotted slot per the assembly program. This extra step helps in validating the placements of the components and improves the turnout rate for a successful production.

All aspects of reflow also must be amenable to improve solder performance and the same translates to our guideline where only the most recent batch of solder paste (with most activity) is permitted for use, which is validated by FAI. Apart from pre-reflow FAI, post-reflow X-Ray also helps validate the solder performance based on the reflow profile which can then be adjusted accordingly so that all components are successfully soldered. This can be similarly implemented at the rest of the printed circuit board assembly stages as well up to testing. But there is a necessity to establish a constant groundwork or point of reference in such a dynamic process to give each validation at a particular stage, the perspective of what changes were made before. This is achieved by using a single piece of documentation used to validate at every stage, wherever applicable, and that document reports any changes made to the processes or product, to the next stage.

pcb_assembly
pcb_assembly

PNC employs the use of AEGIS software to combine SMT assembly guidelines and inspection requirements into a single document (internally referred to as AEGIS). The AEGIS is used to report every single FAI validation to different stages of assembly. PNC’s FAI process for SMT starts with thorough solder paste FAI & its validation, which will be detailed in another post. For this post, let us consider pre-reflow FAI and highlight its validation process since it is the most crucial stage. The procedure is as follows:
1. The SMT team confirms the correct allocation of components as given in the assembly program. This is done by comparing each component with its description, measuring component value wherever applicable, and checking for physical marking on ICs. This helps in validating that the right component has been placed in its respective position on the board.
2. The next step involves checking for the polarity of components, wherever applicable. This is a two-step process. First, the supply angle of a component in the reel needs to be checked and second, the placement of that very component on the PCB needs to be verified.
3. Now, once the first board is assembled, the pcb assembly is put through FAI, where the placements of all components on the board are checked, any necessary placements that remain are placed manually and polarities of applicable components are checked and changed as per what is given in the AEGIS. The same changes are made in the assembly program to avoid the same occurrence in the rest of the batch. Components that are designated as DNP (Do Not Place) are also checked and finally, the solder paste information such as solder type, lot number, date of manufacture, and expiry are checked to ensure that the right solder paste has been used.
4. All these checks translate to notes, remarks, and checks on the AEGIS document, which can then be referred at later stages up to final inspection. If the job in consideration is a repeat job, it can be optimized to avoid any errors made in the first batch of production.
5. The board is then sent through reflow. Once reflowed, the board is extensively inspected under high magnification camera for quality of component placement, solder joints etc. yielded by SMT process.
6. Each section in the AEGIS is meant for FAI by a different team performing a different operation.

PNC has been able to reduce its lead time and increase customer satisfaction significantly and our personalized and successful FAI is a big factor contributing towards it. Further development to the FAI process is underway as much as it is needed to achieve better production yield over time for all the different types of PC Board assembly that are assembled at PNC.

solderpaste

Basics of Solder Paste selection for PCB Assembly

INTRODUCTION

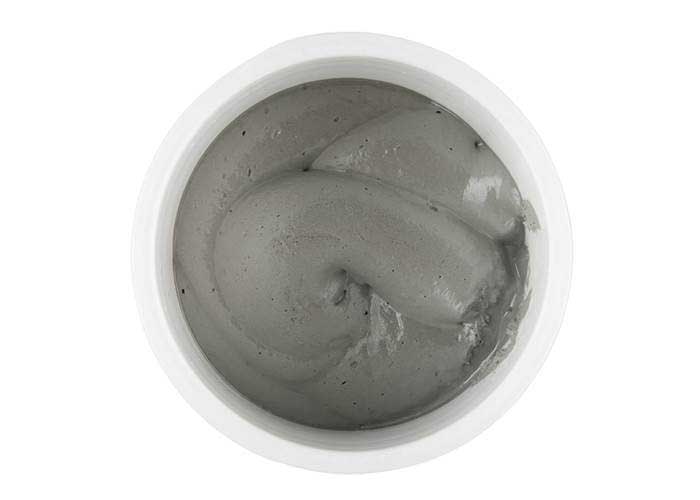
Solder pastes are amorphous putty-like soldering materials used to solder surface-mounted components to the Printed Circuit Board. The effect of solder paste on the PCB’s structural and functional integrity is the paramount factor to consider when deciding on selection of solder paste for application. Many factors which contribute towards the strength of the solder joint and its conduction efficiency need to be addressed as well. This is not just a discussion on what measures and precautions to take during PCB assembly and reflow, but also to put into question what a PCB design engineer should consider when designing a PCB and how the layout should adapt to the corresponding solder paste properties to yield the best result. It is a very brief introduction towards an expansive topic like solder pastes which will be discussed in further detail in future posts.

PROBLEM STATEMENT

A big concern for manufacturers arises when they need to select the right solder paste for SMT applications that is best suited to the PCB assembly and the manufacturing setup. A regular PCB has different types of components, all of which cannot always be compatible with the one solder paste applied across the board and thus, need some necessary compromises in solder selection. PCB designers should be educated about solder paste application and properties in SMT manufacturing to increase reliability of product yield.

SOLDER PASTE BASICS

Solder pastes are categorized based on the following characteristics: RoHS compliance (solder composition), flux type, grain size etc. RoHS (Restriction of Hazardous Substances) is a directive which mandates the exclusion of lead and other hazardous materials from solder pastes and manufacturing processes and aims to reduce environmental and occupational hazards related to electronics manufacturing. It has been adopted as a standard for commercial applications while only military applications can use leaded manufacturing processes. Many components now specifically require RoHS or non-RoHS procedures for PCB Assembly.
Flux is a chemical resin that is used to facilitate the soldering process. It is responsible for removing dirt and preventing oxidation of the component tips during reflow. They can be classified as either water-soluble fluxes or no-clean fluxes. Water soluble fluxes can be cleaned by using water while no-clean fluxes produced low levels of residue which are not necessary to clean but it is advised to clean with designated chemical wash to provide better result.
Solder pastes consist of solder grains which are available in different sizes which are given numerical designations from Type 1 to Type 8 based on descending order of solder grain sizes. Decrease in solder grain size also highlights the advancements in solder technology where Type 1 was adopted first, and Type 8 is the latest addition to minimum achievable solder grain size.

SOLDER PASTE

Since 2006, commercial solder pastes were manufactured and used without lead and other hazardous materials like cadmium and mercury in accordance with the RoHS directive. The directive also affected key PCB fabrication processes and successfully eliminated usage of hazardous materials for commercial applications. Lead in a traditional tin-lead alloy solder is responsible for lowering the melting temperature of the solder to approx. 183°C and it also helps slow down the rate of tin whisker growth in electronics. The process of finding replacements to maintain those advantages offered by lead is still ongoing. Lead-free solders have higher melting points and are more expensive than leaded solders.
The most popular lead-free solder currently being offered is tin-silver-copper alloy which has a melting temperature of approx. 217°C. This has also resulted in components like resistors, transistors being conformed to RoHS compliance. The main drawback of maintaining RoHS compliance for the product is that it is significantly more expensive than leaded processes and does not yield any benefits of switching to lead-free options. The effect of RoHS directive on component manufacturing and the larger effect on electronics manufacturing will be discussed in detail in future posts.
As of today, Type 3 solder is the most widely used solder paste. The following comparison consists of certain superficial characteristics which are a good point to start at before diving into a thorough discussion for each and exploring more complex properties and features of solder pastes. The reason behind comparing T3, T4 and T5 specifically is that T4 and T5 were recently adopted for mass usage for finer and smaller footprints in the PCB assembly industry while T3 has been the industry standard for a long time.

solder paste
solder paste

It is important to note that the sensitivity and reactivity of solder paste to temperature change increases as the solder grain size decreases. This is due to increase in the number of solder grains occupying the same area as the solder grain size decreases. Simply put, the greater the number of solder particles in a given area, the more reactive that particular area of solder will be. Therefore, from this we can conclude that T4 solder will melt at a lower temperature than T3, and T5 will melt at a lower temperature than T4. The advantages, disadvantages and the various effects of using small grain-size solders on component structure and performance will be discussed in further detail in the next post.

FLUX

Fluxes are infused in the solder paste and they are released during reflow. The flux is always released before the solder can melt to provide an oxidation-free environment. Its chemical profile consists of a natural or synthetic resin to coat the component pins and pads, activators to release the flux at the right temperature, solvents to facilitate deposition of solder on the joint, and additives to compensate for any modifications in flux composition. Water-soluble and no-clean fluxes are both used in various situations based on the amount of oxidation occurring during reflow, the level of reactivity of the solder, solder grain size, material of the board, and surface finish of the board.
solder_paste
No-clean fluxes are generally used for boards where the corrosion resistance of the surface is weak. It yields low residue on the printed circuit board assembly because the flux either burns off during reflow or it forms noncorrosive, localized residue around the solder joints. Contrary to its name, it does require cleaning post-reflow but less so than most other high-residue fluxes. No-clean solder pastes are used as an industry standard by most electronics manufacturing service providers because of its ease of use. The main drawback of using no-clean flux is that since it is less corrosive, it does not provide as much protection from oxidation as water-soluble flux but that has to be accepted as a trade-off for better quantitative results in large-scale production.
Water-soluble fluxes are generally used for precise action and give excellent results but the main drawback is that they require careful application and condition regulation due to their highly reactive and corrosive nature, and the difficulty in cleaning them post-reflow. Compared to no-clean flux, it produces more residue that cannot be removed easily from the board and due its high corrosivity, it may damage the PCB surface and component leads. Cleaning unwanted residue off the board requires additional machinery which occupies valuable space on the shopfloor. This limits its usage in the industry to only customer requests or specifications to use water-soluble solder pastes.

KEY CONSIDERATIONS FOR PCB DESIGNING

It is important to consider how solder selection will affect your PCB design. For simplicity, the effects will be divided based on solder paste composition, solder size and flux usage. Many of these considerations may overlap or may have to be used in conjunction for achieving the best result.

SOLDER PASTE COMPOSITION:

• Components used on PCB should be first checked to see if they are RoHS compliant or not, based on the solder paste used. Components with RoHS compliance usually have different leads which may or may not be compatible with leaded solders, and it may affect the solderability of the component to the copper pads, the solder joint’s mechanical strength, and component shelf-life and performance. It is also important to ensure the components operating and manufacturing parameters meet the solder paste properties, otherwise components may get burned or dysfunctional during the reflow process, leading to visible or latent component failure.
• Flux selection should be based on solder paste composition. Flux release at specific temperatures should be done in conjunction with the reflow profile for that specific solder paste. Solder melting and flux activation occur at different instances in the reflow process. Early activation of flux may cause surface corrosion, component failure, early burn-off which may lead to poor soldering and late activation may lead to increased oxidation during reflow process along with difficulty in cleaning.

SOLDER SIZE

• Solder grain size should also be considered when choosing component package and its corresponding design footprint on the Printed Circuit Board. Larger footprints do not require smaller grain-size solders. If the grain size is small, say T5, then based on its high reactivity, more number of particles per unit area and greater wetting ability, solder may flow too easily on melting resulting in solder defects which will affect component performance and product life-cycle. The reverse situation, where small footprints are used in conjunction with large grain-size solders, also leads to solder defects.
• Component package selection will also affect stencil aperture size, stencil thickness and solder deposition efficiency. Using large-size solders, say T3 solder, for micro-BGA or 01005-imperial sizes will result in gasketing and insufficient paste deposition; while using small-size solders, say T5 solder, for large footprints may result in bridging.
• The spacing between footprints of separate components, spacing between component leads of the footprint on the Printed Circuit Board should change based on the solder grain-size as using large grain sizes for small footprints, and vice versa, will lead to solder bridging which will in turn affect device performance and life-cycle.

FLUX COMPOSITION

• PCB thickness, material and coatings should be selected based on flux used for the reflow process. One should avoid using water-soluble fluxes for a thin PCB as they are highly corrosive in nature and may lead to excess surface corrosion. Corrosion resistant material and coatings should be used in accordance with the flux selected, as not using them will lead to corrosion and cleaning issues and using them when not needed(say a no-clean flux is being used) will increase cost of production.

All PCB’s should be designed keeping in mind the effects of solder paste, stencil design, flux, process used on
SMT assembly
PCB’s. Some of these topics and more will be added to the list and discussed in further detail in the future.

CONFORMAL-COATING

CONFORMAL COATING

What is Conformal Coating?

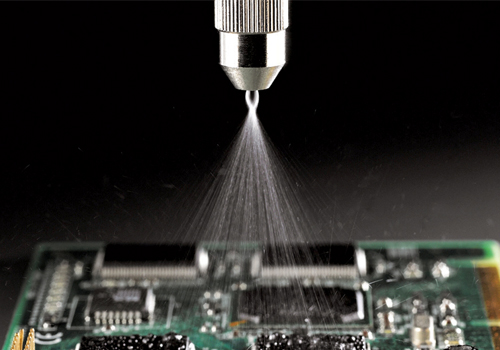
Conformal coating is protective chemical material coating applied after the final SMT PCB assembly or through-hole assembly process. Coatings are comprised of 5 different types, Acrylic, Epoxy, Urethane, Silicone and Parylene resins. Applying the coatings to a PCB board assembly can be done by hand spray, robotic spray, brush or dipping. The coating acts as an additional dielectric layer that provides protection due to environmental and mechanical stresses, such as thermal extremes, chemicals, dust, salt fog, abrasions, and moisture. In a PCB assembly that has close spacing of conductive pathways or close spacing of components the coating will help minimize dendrite growth over a period of time that causes shorting.

conformal_coating

Robotic Spray vs Traditional applications:

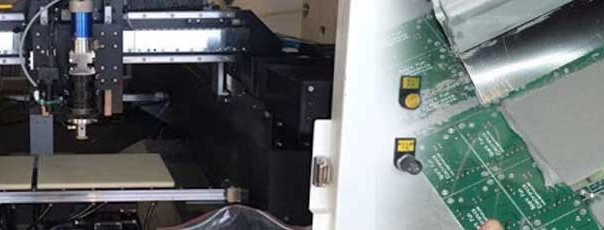
The method of application will depend on the customer requirements of the turnkey pcb assembly, but PNC prefers spray method for consistency in overall coating thickness. There are often select components on a pcb board assembly that will not be required to be coated. The traditional way is to block out or mask the selected components with tape. This is time consuming, costly and a possibility that the component can be damaged on the SMT assembly when removing. The robotic method can be programmed accurately to spray around the parts thus ensuring no component damage from masking and maintain a repeatable coating thickness.

When choosing a conformal coating for your turnkey pcb assembly, there are many manufacturers to choose from. The following are a few that we work with, Dymax, HumiSeal, Dow Corning, Hysol, Loctite, and Huntsman. Based on your application and environment of your PCB assembly, choose the Type of coating that fits the PCB board assembly, by visiting their web pages to find the strengths and weaknesses.

IPC J-STD-001D Conformal Coating thickness requirements

Type AR Acrylic Resin 0.03 – 0.13 mm (0.00118 – 0.00512 in)
Type ER Epoxy Resin 0.03 – 0.13 mm (0.00118 – 0.00512 in)
Type UR Urethane Resin 0.03 – 0.13 mm (0.00118 – 0.00512 in)
Type SR Silicone Resin 0.05 – 0.21 mm (0.00197 – 0.00827 in)
Type XY Parylene Resin 0.01 – 0.05 mm (0.000394 – 0.00197 in)